Barcode verification requirements should be written as a controlled part of the label specification, not as a vague request for a code that “scans” or has a “good grade.” A usable requirement identifies the barcode symbology, encoded data, applicable verification method, minimum acceptable grade, verifier configuration, production sampling plan, and response when results fall below the agreed limit.
This matters because a label can decode on one scanner and still fail a formal verification requirement. Conversely, a verified symbol may still have problems in a particular field environment if it is damaged, obscured, curved around a container, scanned at an unsuitable angle, or exposed to contamination. Barcode quality is therefore one element of a wider label and application system.
Start with the barcode application, not a generic grade
The first question is not “What grade should this barcode achieve?” It is “What barcode is required for this application, and whose rules apply?”
Identify the following before setting a grade threshold or buying a verifier:
- Symbology: for example, EAN/UPC, GS1-128, Code 128, Data Matrix, GS1 DataMatrix, QR Code, or another defined symbol.
- Encoded data: the approved number, identifier structure, application identifiers, serialisation data, lot number, expiry date, or other required content.
- Code owner or application system: a retailer, brand owner, logistics customer, healthcare programme, traceability scheme, or internal manufacturing system may define additional rules.
- Label use: retail point of sale, warehouse logistics, work in progress, asset identification, medical-device labelling, industrial traceability, or consumer engagement.
- Scan environment: handheld scanner, fixed-position reader, point-of-sale scanner, mobile device, vision system, or another reading system.
- Final surface and use conditions: flat or curved application, abrasion risk, condensation, refrigerated storage, chemical exposure, overlamination, and expected handling.
For symbols governed by GS1 rules, the relevant GS1 application guidance should be checked alongside the artwork and customer requirements. A symbol type alone does not establish all acceptance conditions. A GS1 DataMatrix used in one supply-chain application, for example, may be subject to different data and quality expectations from a visually similar Data Matrix used for internal manufacturing control.
Do not assume that a customer’s phrase such as “ISO compliant barcode” is complete. Ask which symbol, which application standard or customer manual, what verification method, what grade basis, and what production records are required.
Scanning and verification answer different questions
Scanning is a functional test. A scanner attempts to decode the data from a symbol under that scanner’s optics, software settings, lighting, distance, angle, and handling conditions. This is useful for confirming that a label works with the intended reader or a representative reader population.
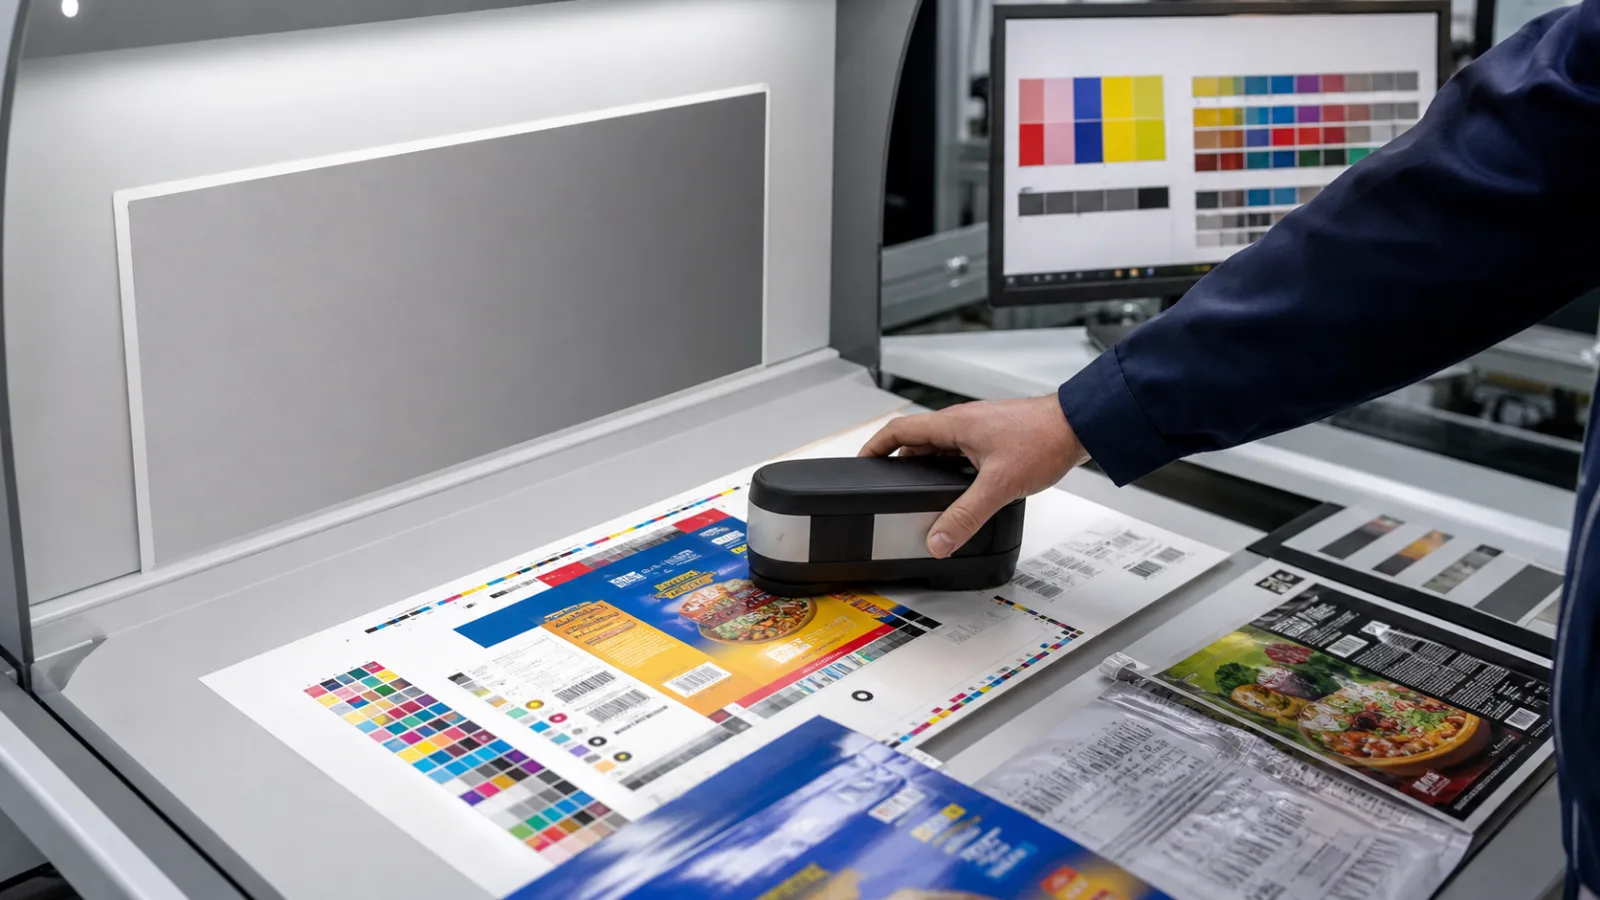
Verification is a controlled measurement process. A calibrated verifier evaluates a barcode against a specified print-quality method and reports a grade, usually with parameter-level information that can help identify the cause of reduced quality. The result is meaningful only when the report also identifies the method and measurement conditions used.
In practical terms:
| Check | Main question answered | Typical limitation |
|---|---|---|
| Scanner read test | Can this reader decode this label in this test condition? | A successful read does not establish a formal verification grade. |
| Barcode verification | Does the symbol meet the stated quality method and grade under defined conditions? | A passing grade does not guarantee reading in every real-world environment. |
| Vision or process-control inspection | Is the code present, positioned correctly, and carrying expected data? | It may not provide an ISO-based print-quality grade. |
Some production systems combine data validation, presence inspection, and barcode quality measurement. These functions should still be specified separately. Manufacturer guidance also distinguishes application-specific grading from general reader-based process control; for example, Cognex describes verification as grading codes to specified standards and notes that application standards can add their own requirements.
A read test remains valuable where the field scanner, label geometry, or product presentation creates a specific risk. It should supplement, not silently replace, the agreed verification requirement.
Match the symbol to the applicable verification method
A barcode verification specification must distinguish between linear and two-dimensional symbols.
For conventional printed linear barcodes, ISO/IEC 15416 is the commonly referenced barcode print-quality test specification. For two-dimensional symbols, ISO/IEC 15415 is the corresponding commonly referenced print-quality test specification. Their scope, measurement parameters, illumination conditions, aperture or sampling settings, and reporting conventions are not interchangeable.
This distinction is important because a linear symbol is assessed through scan reflectance profiles, while a matrix symbol is evaluated through its grid, modules, fixed patterns, contrast, error correction and other two-dimensional characteristics. A report described simply as “ISO verified” gives too little information to establish which method was used.
Direct-part marking can add another layer of complexity. Marks on metal, moulded plastic, curved parts, textured surfaces, or reflective components may require an application-specific method or a verifier designed for direct-part-mark conditions. Do not apply a printed-label requirement to a direct-part mark without confirming the governing requirement.
The specification should name:
- The exact symbology and intended application.
- The verification method required for that symbol type.
- The required measurement condition where the method or application specification calls for it.
- The verifier model or approved verifier capability.
- The required report format and grading basis.
Check the current published edition and scope of the relevant ISO/IEC document before release. The standard edition, customer requirement, and verifier documentation need to align. A verifier may support several code types but not every illumination, aperture, direct-part-mark mode, or reporting configuration required by a particular job.
Write the requirement as a controlled job specification
A barcode requirement should be readable by the buyer, artwork team, label converter, printer operator, and receiving quality team. It should also prevent a later dispute over whether the converter was asked to demonstrate readability, data correctness, formal grading, or all three.
A concise requirement block can include the following fields:
- Symbol: identify the exact symbology, such as GS1-128 or Data Matrix.
- Data rule: state the approved data source, data format, check-digit rule where applicable, and whether human-readable text is required.
- Artwork location: define orientation, placement, nominal size, quiet zones, exclusion areas, and any permitted rotation.
- Verification method: name the applicable test method and any application-specific requirement.
- Minimum grade: state the agreed grade and the basis on which it is expressed. Do not use “scan grade” as a substitute for a defined method.
- Verifier setup: identify the approved verifier, relevant configuration, illumination condition, aperture or measurement setting where applicable, and calibration status requirement.
- Acceptance sample: identify whether results apply to first-off labels, retained samples, production samples, or every inspected label.
- Records: define the report fields, file format, lot reference, date, operator or system identification, and retention period.
- Nonconformance action: state who must be notified, whether production may continue, what containment is required, and how rework or release is authorised.
The minimum grade should come from the applicable application standard, customer specification, quality agreement, or contract. ISO/IEC verification methods describe how quality is measured; they should not be treated as a universal instruction to use one grade threshold for every label application.
Specify sampling, records, and escalation separately
A verification method is not a production-control plan. The method defines how a selected symbol is measured. The production plan defines which labels are selected, when they are checked, how results are recorded, and what happens when performance changes.
A practical plan usually separates approval, routine control, and escalation.
- Approve the final construction. Verify representative labels made with the intended facestock, adhesive construction, ink or ribbon, print process, varnish, laminate, and any subsequent finishing. A proof printed on a different material or process may not represent production performance.
- Approve first-off production. Check the first acceptable production labels after setup or changeover against the agreed requirement.
- Define routine sampling points. Sampling may be linked to roll changes, press adjustments, material changes, shifts, lot boundaries, or intervals agreed in the quality plan. Frequency should reflect application risk and process stability rather than a generic rule.
- Retain traceable records. Link verification reports to job number, date, lot or roll, machine, artwork revision, label construction, and verifier identity.
- Escalate grade drift. A gradual decline can indicate print growth, ribbon wear, plate degradation, contamination, inconsistent curing, material variation, or a changed finishing condition. Investigate before the result crosses the final acceptance limit where possible.
- Define disposition. Set out whether a failed sample triggers increased inspection, hold of the affected lot, corrective adjustment, re-verification, reprint, customer notification, or another agreed action.
Avoid specifying a universal sample size, verification frequency, or calibration interval unless a controlling customer, sector, or application requirement provides it. These details should be agreed before purchase-order release, especially where barcode quality is tied to chargebacks, traceability, patient safety, or automated distribution.
Control print, substrate, and finishing variables
Verification grades are affected by the final printed symbol, not just the digital artwork. A barcode that appears visually sharp can still have marginal contrast, poor modulation, damaged modules, edge defects, or an unsuitable quiet zone.
Common production variables include:
- Print gain or loss: bars, spaces, modules, and gaps can change from their intended dimensions. The effect depends on print process, plate or screen condition, ink behaviour, thermal transfer settings, and material surface.
- Contrast and reflectance: ink colour, facestock colour, gloss, metallic effects, coatings, and surface contamination can affect the verifier’s measurement.
- Voids and contamination: missing ink, ribbon wrinkles, dust, adhesive transfer, varnish defects, scratches, and abrasion can interrupt bars or modules.
- Distortion: web tension, die-cut registration, shrinkage, label application around a curved pack, and thermal movement can alter the symbol geometry.
- Quiet zones and placement: graphics, text, seams, folds, perforations, container edges, and label curvature can interfere with scanning even where the printed symbol itself is acceptable.
- Finishing layers: overlaminates, varnishes, cold seals, and protective coatings should be included in approval samples. A finish can alter reflectance or introduce glare that changes measured or in-use performance.
When a report shows a reduced grade, do not treat the grade alone as the diagnosis. Review the parameter-level result, compare it with an approved reference sample, confirm verifier calibration and configuration, then inspect the relevant printing and finishing variables. The corrective action should address the cause, not merely chase a higher overall grade.
Pre-production checklist for label buyers and converters
Before release, confirm that the job file and quality agreement answer these questions:
- Is the barcode symbology correct for the application and customer system?
- Is the encoded data drawn from an approved source and validated against the required format?
- Has the applicable barcode verification method been identified for the symbol type?
- Is the minimum acceptable grade stated with its grading basis and measurement conditions?
- Is the selected verifier suitable for the code type, label format, and required configuration?
- Are verifier calibration and setup checks documented under the equipment supplier’s procedure?
- Does the approved sample use the final substrate, ink or ribbon, print process, varnish, laminate, and finishing sequence?
- Are first-off approval, routine sampling, report retention, and lot traceability defined?
- Is there a written response for failed samples, grade drift, and disputed results?
- Has a representative field read test been added where the intended scanner or application environment creates additional risk?
Specify barcode verification as a controlled agreement between the data owner, label buyer, converter, and receiving party. The most defensible requirement is not the highest possible grade stated without context; it is the correct method, configuration, threshold, sampling plan, and record set for the symbol’s actual application.
Sources
- What is Barcode Verification and Grading?
- Verification of barcodes
- Application Standards for Barcode Verification
- Barcode Verification Explained: Barcode Grading, and Why Barcode Quality Matters
- Barcode Verification and Grading
- TSC Printronix Auto ID launches a thermal barcode label printer capable of printing and encoding RFID labels and inspecting to ISO quality standards in a single pass